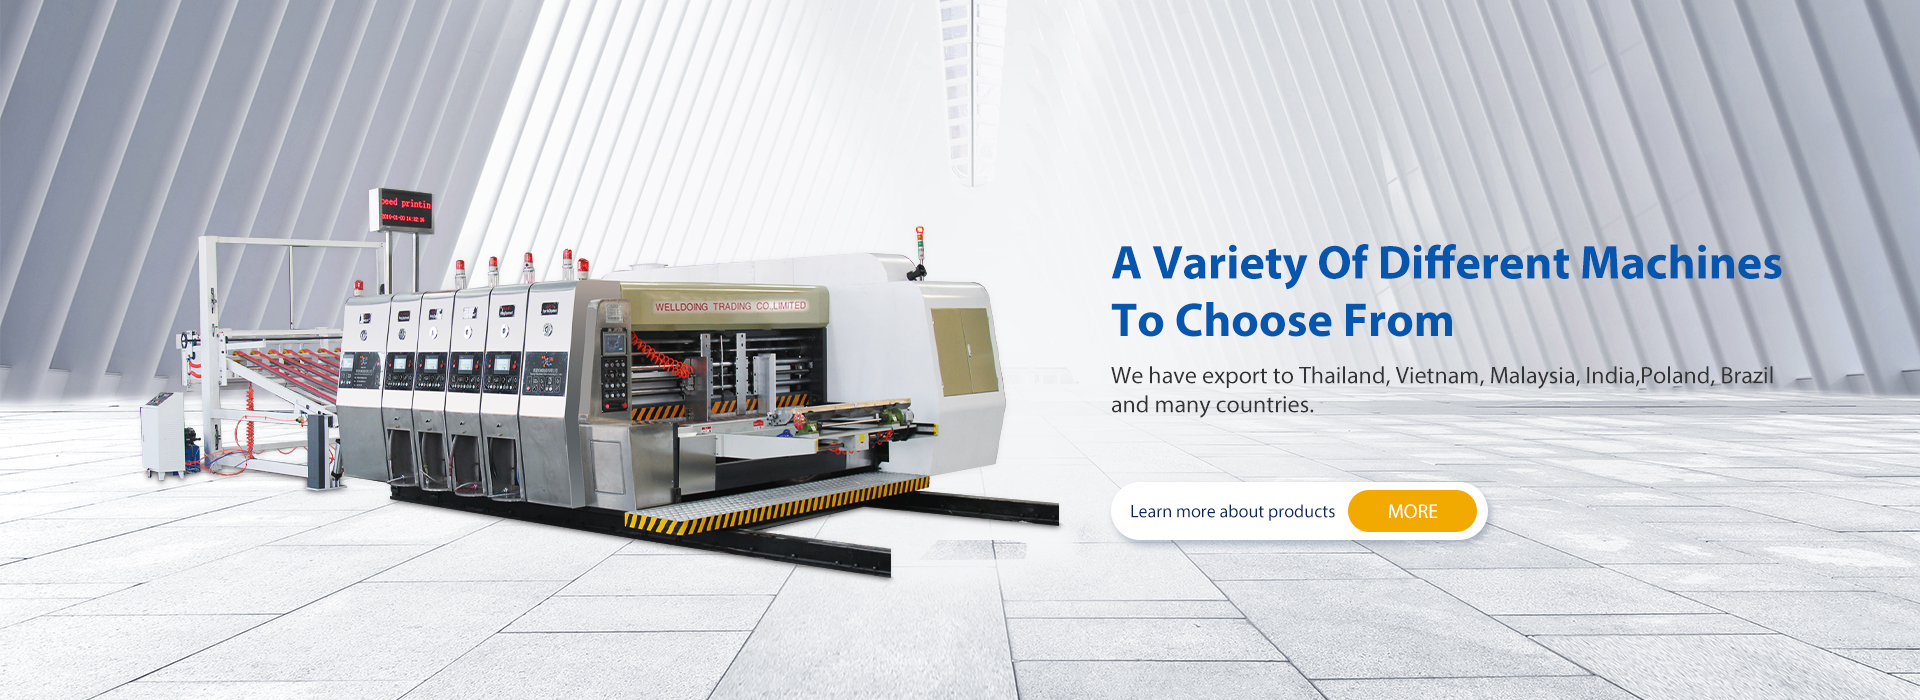
A flexo printer slotter die cutting machine is the core production line for corrugated carton factories. It integrates feeding, flexographic printing, slotting, creasing and rotary die cutting in one unit, widely used for custom shipping boxes, packaging cartons and display boxes. Many carton manufacturers face frequent unplanned stops, blurred printing, uneven slotting and rough die cuts simply because they lack standardized maintenance for their flexo printer slotter die cutting machine. Good preventive maintenance does not only stabilize print and die-cut quality, cut corrugated board waste, but also greatly extend the service cycle of your flexo printer slotter die cutting machine and lower long-term operation cost. This guide sorts out actionable maintenance plans, key component inspection standards and common mistakes for operators and maintenance engineers.
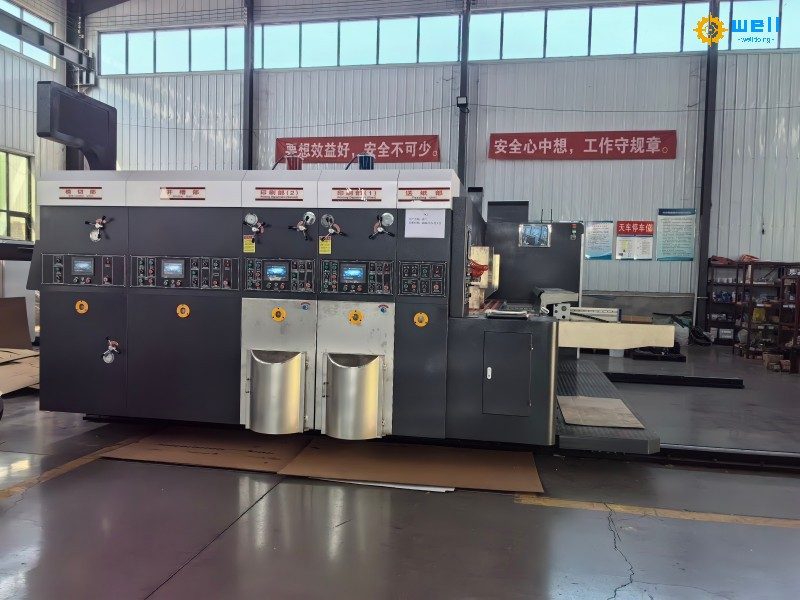
Daily maintenance after each shift
Daily maintenance is the foundation for stable running of a flexo printer slotter die cutting machine, and it should be finished before machine shutdown every day. First, clean the flexo printing unit. Flush ink pans, ink circulation pipes, ink pumps and doctor blade chambers with manufacturer-approved water-based ink cleaner. Remove dried ink residue from anilox rolls and printing plates. Never use hard scrapers or wire brushes, which will scratch the anilox cell structure and damage flexible printing plates, leading to light print, missing patterns and unstable color registration. Wipe the surface of plate cylinders and check doctor blades for bending, nicks or uneven wear. Replace damaged doctor blades in time to avoid streaks on printed cartons. Second, clear paper scraps, corrugated dust and glue residues inside the slotting station and die cutting station. Clean slotting wheels, creasing rollers, rotary die rules and anvil covers. Built-up paper debris will cause crushed board, inaccurate creasing and burrs on die-cut edges. Check the feeding conveyor, suction feeder and paper guide rails. Remove dust on sensors, photoelectric eyes and registration cameras; dirty sensors are a top cause of feeding skew and print registration deviation on flexo printer slotter die cutting machine. Third, carry out visual inspection. Listen for abnormal noise from gears, chains and bearings. Check air pressure of the pneumatic system, look for air leakage at joints and cylinders. Confirm emergency stop buttons, safety guards and interlock switches work normally. Top up lubricating oil at specified points if oil level is low, and record abnormal conditions in the maintenance log.
Weekly maintenance for flexo printer slotter die cutting machine
Weekly maintenance goes deeper into transmission systems and precision alignment, suitable for low-production shifts every week. Lubricate all moving parts strictly following the lubrication chart: drive chains, sprockets, bearing seats, linear guide rails, slotting shaft bearings and die cylinder bearings. Use the specified grease or hydraulic oil; mixed oil types will accelerate bearing corrosion and gear wear. Adjust tension of timing belts and conveyor belts. Loose belts cause slipping, feeding speed fluctuation and inconsistent printing pitch. Over-tight belts shorten belt lifespan quickly. Check alignment and registration of the whole flexo printer slotter die cutting machine. Run a test corrugated board sample to verify print registration, slotting position and die cutting position. After frequent job changeover for different carton sizes, servo parameters and mechanical positions tend to drift. Calibrate the registration system and reset compensation values when offset appears. Inspect slotting knives, creasing wheels and rotary die cutting rules. Sharpen dull slotting blades and die cutting steel rules. Check anvil cover wear; rotate or replace the anvil cover once obvious grooves appear, otherwise it will crush the flute of corrugated board and produce poor die-cut quality. Tighten loose fasteners on each unit, including cylinder fixing bolts and die plate locking screws. Clean dust inside electrical cabinets with dry compressed air; moisture and dust are the main triggers of PLC and servo drive faults.
Monthly & quarterly preventive maintenance
Monthly and quarterly maintenance focuses on wearable core components and system performance testing of carton box printer die cutter slotter equipment. Send heavily contaminated anilox rolls for ultrasonic cleaning monthly to recover ink carrying volume. Test cell volume regularly. When cell volume drops beyond the allowable range, recoat or replace the anilox roll. Check ink filter elements and pneumatic filter elements, replace blocked filters to keep ink circulation and air supply clean. Check gear backlash, bearing clearance and shaft runout of the printing, slotting and die cutting units. Measure the parallelism between die cylinder and anvil cylinder. Uneven clearance leads to partial over-pressure cutting and partial incomplete cutting. Inspect all solenoid valves, pressure regulators and servo motor cables. Replace aging seals and cracked cables before sudden failure. Quarterly, run a full machine performance test. Record feeding speed range, registration accuracy, die cutting repeat tolerance and energy consumption. Compare data with baseline records to find hidden degradation. Back up PLC program and touchscreen parameters for your flexo printer slotter die cutting machine, which saves much recovery time after electrical failure.
Annual overhaul and spare parts management
Arrange a full annual overhaul during production off-season. Disassemble, inspect and overhaul heavy-load transmission assemblies, replace severely worn bearings, gears and chains. Check the frame level of flexo printer slotter die cutting machine and re-level if the foundation sinks, because uneven frame directly destroys the coaxiality of all rollers. Build a scientific spare parts inventory for flexo printer slotter die cutting machine. Stock consumables: doctor blades, anvil covers, slotting knives, belts, filters, sensors, seals and printing plates. Keep critical spare parts on hand to cut waiting time when breakdown happens. Store rotary dies and printing plates in dry, flat storage racks to avoid deformation and rust.
Common maintenance mistakes to avoid
Many carton operators damage flexo printer slotter die cutting machine by wrong habits. Do not skip cleaning to rush production; dried ink will permanently block anilox cells. Do not over-adjust die cutting pressure to chase clean cuts; excessive pressure crushes corrugated flutes and speeds up die and anvil wear. Do not use unmatched lubricants or ignore maintenance logs. Do not remove safety interlocks for faster job changeover, which brings serious safety risks.
Final summary
A flexo printing die cutting slotting stacker machine china delivers stable output, high carton quality and low ownership cost only with layered, documented maintenance. Daily cleaning and inspection stop small problems; weekly calibration and lubrication preserve precision; periodic overhaul prevents catastrophic breakdown. If you are sourcing a reliable flexo printer slotter die cutting machine for your corrugated box plant, our well-built machine adopts heavy-duty frame, stable servo feeding and easy-access structure, designed for convenient daily maintenance and long continuous running. A well-maintained flexo printer slotter die cutting machine is the most reliable asset for your packaging factory.
Email:cartonmachine.tomwang@aliyun.com
Phone/Wechat/Whatsapp:+86 133 0307 8975
Post time: Oct-22-2026